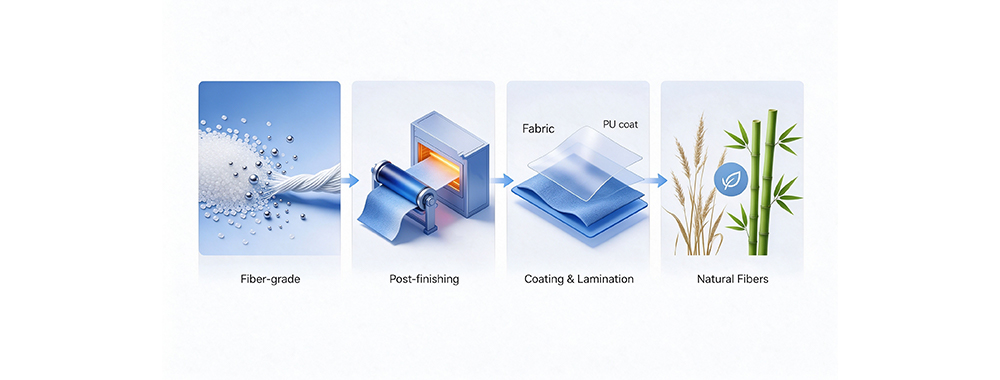
Antimicrobial fabrics are made in three primary ways: antimicrobial agents such as silver ions, copper and zinc are blended into the raw material at the fiber-manufacturing stage, giving the fiber itself antimicrobial properties; an antimicrobial finish is applied after the fabric is woven, through padding or coating processes; or a coating or film containing antimicrobial actives is laminated onto the fabric surface. In addition, natural fibers such as bamboo and hemp exhibit inherent bacteriostatic properties of their own.
If you have ever checked the labels while choosing a gym bag, backpack or travel case, you have likely come across terms like “antimicrobial fabric,” “odor-resistant” or “antibacterial lining.” But what do these claims actually mean?
As an OEM/ODM bag manufacturer, Synberry works with antimicrobial textiles every day. In this article, we break down the principle, pros and cons, compliance requirements and practical applications of each process in custom bag manufacturing.
Ⅰ. Antimicrobial Fabric: Definition and Technical Boundaries
Ⅱ. Four Manufacturing Processes for Antimicrobial Fabric
Ⅲ. Quality Control and Testing Standards: How to Verify Antimicrobial Fabric
Ⅳ. Regulatory Compliance for Antimicrobial Fabric
Ⅴ.Practical Applications of Antimicrobial Fabric in Bag Manufacturing
Ⅵ. Frequently Asked Questions (FAQ)
Ⅶ. Conclusion
Antimicrobial fabric is a textile that has been treated or specially manufactured to inhibit the growth of microorganisms such as bacteria, fungi and mold. Rather than masking odor, its job is to reduce the microorganisms that cause it at the source.
Two concepts are often confused and need to be clarified first:
Understanding this distinction is essential for choosing the right test standards and interpreting test reports correctly.
This is one of the most durable processes: treatment is applied at the fiber or yarn stage — before weaving. Antimicrobial agents (such as silver, copper and zinc compounds) are added directly to the polymer during fiber extrusion.
Another common approach is to apply an antimicrobial finish after the fabric has been woven. The fabric passes through a padding bath or coating rollers to pick up the finishing agent, and is then dried and cured at high temperature.
Common finishing agents include:
Note: Finishing is lower in cost, but its laundering durability is weaker than fiber-level treatment — performance gradually declines with each wash cycle.
For the bag industry, this is the most practical and widely used approach. A thin antimicrobial coating or film is laminated onto the bag’s lining or outer fabric — often completed in the same production step as a waterproof coating or PU coating.
Because it can be embedded directly into existing production lines, it is highly cost-effective and scalable for high-volume custom manufacturing.
Some fibers are inherently antimicrobial and require no chemical additives:
It is worth noting that copper-ion fiber, though commonly used in antimicrobial textiles, is a modified man-made fiber with copper ions embedded inside during spinning — not a natural fiber.
Natural fibers used alone usually fall short of stringent antimicrobial standards, but they can be combined with other processes while appealing to environmentally conscious consumers. In practice, a “natural fiber + physical antimicrobial finish” combination is often adopted.
A fabric must pass standardized testing before it can truly be called “antimicrobial.” The most frequently cited standards include:
• AATCC 100 (US textile antibacterial test standard): uses the shake flask method to calculate the 24-hour antibacterial rate. In commercial practice, an antibacterial rate of ≥90% is commonly used as the effectiveness threshold; this figure is not a mandatory pass/fail criterion in the standard text.
• ISO 20743 (international standard for evaluating antibacterial activity): uses the quantitative absorption method to determine the antimicrobial activity value. The industry generally agrees on R ≥ 2.0 (a 2-log reduction) as the commercial threshold for effectiveness; this threshold is likewise not a mandatory provision of the standard.
• JIS L 1902 (Japanese Industrial Standard): covers both quantitative (bacterial suspension absorption) and qualitative (zone of inhibition) methods. The standard was in fact revised from ISO 20743, and the quantitative test methods of the two are consistent.
Key insight on these standards: the three standards differ in test organisms, inoculation methods, contact times and how results are expressed, so they cannot be compared directly. For example, AATCC 100 expresses results as a percentage reduction, ISO 20743 as an antimicrobial activity value (log reduction), and JIS L 1902 may involve both qualitative zones of inhibition and quantitative activity values. Brands should select a test standard based on their target market and customer requirements.
These tests assess effectiveness by measuring the log reduction of bacteria. For instance, “kills 99.9% of bacteria” corresponds to a 3-log reduction against Staphylococcus aureus or E. coli, with a test contact time of typically 18–24 hours.
Durability testing is carried out with wash cycles per ISO 6330. ISO 6330 only defines the washing procedure and does not set a pass line for antimicrobial performance; however, many brands’ internal specifications and some industry guidance standards require that ≥80% of the antibacterial rate be retained after 50 washes — a technical threshold agreed between customers and the industry.
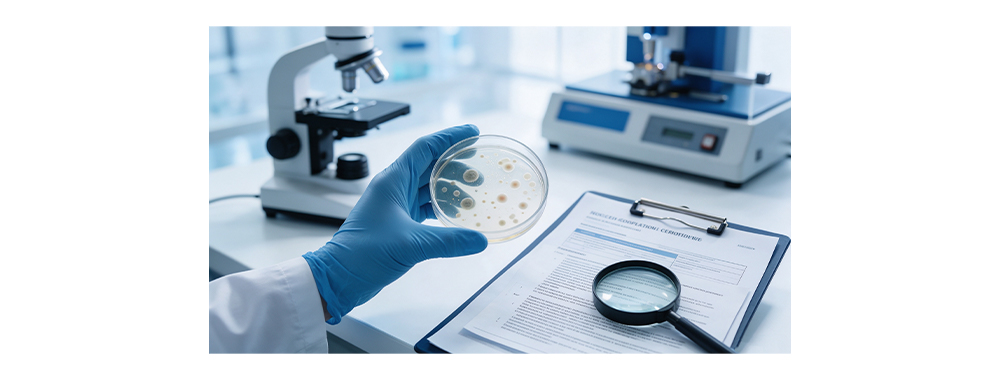
This is the most easily overlooked yet most important step in purchasing decisions. Antimicrobial textiles are subject to dedicated regulations in every major market around the world — the days of launching a product on the word “antimicrobial” alone are over.
The EU Biocidal Products Regulation (BPR, EU No 528/2012) came into effect on September 1, 2013, formally bringing "articles treated with biocidal products" under regulation.
Under the BPR, antimicrobial-treated textiles sold in the EU market must only be treated with approved active substances. More importantly, if the antimicrobial function is claimed as the product’s primary function, the product may be classified as a “biocidal product” rather than a “treated article,” which triggers a more stringent authorization procedure.
At present, some traditional silver-based active substances are in the review process of ECHA (the European Chemicals Agency) and face the risk of non-approval. Not all silver-ion technologies will be banned; the industry is actively developing BPR-compliant alternative antimicrobial solutions.
In the United States, treated articles with antimicrobial functions are regulated under the Federal Insecticide, Fungicide, and Rodenticide Act (FIFRA). Under FIFRA, products that kill or repel bacteria or germs are pesticides and must be registered with the EPA before they can be sold.
However, FIFRA provides an exemption for “treated articles”: if the antimicrobial agent is used solely to protect the article itself (for example, preventing the fabric from degrading or developing odor due to microbial activity), and no public health claims are made (such as “prevents the spread of bacteria” or “reduces virus exposure”), the article can be exempt from registration. The prerequisites are that the antimicrobial active substance itself must already be EPA-registered for the intended use, and the product must not make claims beyond the scope of the exemption.
Beyond the BPR and FIFRA, the following also deserve attention:
• The EU REACH regulation restricts the chemicals used in antimicrobial agents;
• California Proposition 65 requires a reproductive toxicity warning when silver exposure from a product exceeds the safe harbor threshold (the relevant requirements took effect in 2025; products meeting the exemption threshold are exempt from the warning);
• Under OEKO-TEX® STANDARD 100 certification, biocidal active substances are prohibited in baby-grade and other mucosa-contact sensitive products; for other product classes, compliant biocidal antimicrobial substances are permitted provided their toxicological assessment passes — it is not a blanket ban across all categories.
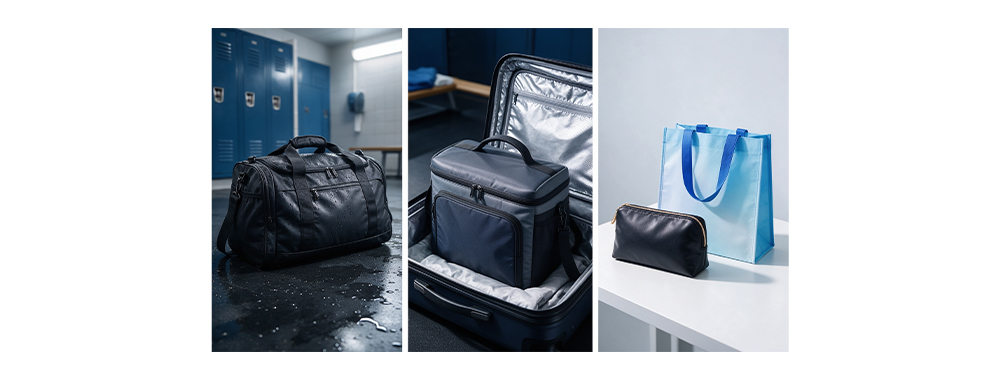
Different bags differ greatly in usage frequency, cleaning methods and exposure environments, which determines the choice of antimicrobial process. As a bag OEM/ODM manufacturer, we typically match processes to the following three scenarios:
These bags pick up sweat easily, and consumers expect frequent cleaning.
In production, fiber-level antimicrobial fabrics (such as yarns embedded with silver or copper ions) or durable finishes with covalently grafted treatments are the top recommendation. These processes ensure that the antibacterial rate remains above 80% even after dozens or even hundreds of washes (tested to ISO 6330).
These bags have damp interiors with poor air circulation, making them highly susceptible to mold and odor-causing bacteria.
In production, the most economical approach is antimicrobial coating and lamination. A coating containing silver-based or quaternary ammonium agents is usually combined with a PU waterproof coating or TPU film in a single lamination step, achieving both water and moisture resistance and microbial control.
These bags are cost-sensitive and are not washed frequently. A low-cost surface padding or spray finish is sufficient to meet basic bacteriostatic needs.
By precisely matching the use scenario, antimicrobial fabric delivers maximum value in bag products while balancing cost, durability and compliance.
A: It depends on the process. Fiber-level treatments (built-in antimicrobial agents) can withstand dozens or even hundreds of washes; surface coatings and non-grafted finishes are less durable, typically showing a marked decline after 20–30 washes. Grafted modifications (such as covalently bonded chitosan or silver-based finishes) significantly improve laundering durability.
A: When compliant with regulations and used as intended, approved antimicrobial fabrics are generally safe to use. The key lies in whether the type and dosage of antimicrobial agents meet the regulatory requirements of the target market, such as the EU BPR/REACH, the US EPA/FIFRA or relevant Japanese standards. Reputable bag manufacturers should be able to provide corresponding compliance documents and safety test reports.
A: Almost any bag exposed to moisture, sweat or bacteria-prone environments is suitable, including gym bags, luggage linings, cooler bags, shoe bags, cosmetic bags, diaper bags, medical bags and school backpacks.
A: Both have their strengths.
Natural fibers are more eco-friendly and skin-friendly, but their antimicrobial strength is limited, and used alone they usually cannot reach the commercial pass thresholds of AATCC 100 or ISO 20743.
Chemical treatments (such as silver ions) deliver stronger antimicrobial performance and can pass standard tests, but some consumers have concerns about their environmental footprint, and regulatory trends such as the BPR’s stance on silver-ion technologies need to be watched.
In practice, a “natural fiber + compliant antimicrobial finish” combination is often adopted.
A: The cost increase depends on the type of antimicrobial agent, process route, fabric weight (GSM) and order quantity.
Generally speaking, antimicrobial coating processes add less cost than fiber-level antimicrobial fabrics (which involve raw-material modification). The actual increase varies significantly from project to project, so we recommend requesting itemized quotations from suppliers on a per-project basis. Large-volume orders can effectively amortize unit costs.
Antimicrobial fabric is not magic; it is built on materials science across three levels: fiber, fabric and coating. Silver-ion antimicrobial linings, coated antimicrobial finishes and natural fiber blends each have their own pros and cons. The best solution is determined by combining the product’s use scenario, the export market’s regulations and the project budget.
| Author | ||||||
|
ぜひ読んで、投稿を続け、購読してください。ご意見をお聞かせください。
著作権
@2024 Synberry Bag & Package Products Co.,Ltd 無断転載を禁じます
.
 サポートされているネットワーク
サイトマップ / ブログ / Xml / プライバシーポリシー